What’s the Maximum Depth of Cut in CNC Die Sinker EDM? A Shop Owner’s Practical Guide for Your Next Project CNC Die Sinker EDM
Let me cut to the chase—when we’re talking CNC die sinker EDM, people always ask one question that’s way more complicated than it sounds: “What’s the maximum depth of cut I can hit on my part?” At our shop, we get this call at least twice a week, usually from guys running smaller job shops or tool and die makers who’ve burned out a dozen electrodes on a deep cavity only to hit a wall. I’ve been doing this for 12 years now, I’ve got three sinkers in the back, and I’ve burned through more copper and graphite electrodes than I can count, so I’m gonna break this down like I’d break it down to a new machinist leaning over my workbench. First, no BS—there’s no universal number. If someone tells you “5 inches max” or “10 inches max,” they’re either selling you a machine they know can’t do that or just guessing. It all depends on a handful of things that matter way more than some random spec sheet.
First, let’s get the basics straight: CNC die sinker EDM works by eroding material with electrical sparks, right? The electrode (usually graphite or copper) never touches the part—you just shoot sparks across a tiny gap (called the spark gap) between them. When you go deep, two big problems pop up: flushing the debris and electrode wear. Debris is all the tiny metal bits that break off your workpiece as sparks eat away at it. If you can’t get those bits out of the hole or cavity, they start arcing between the electrode and the part, which gives you a rough, lumpy finish (we call that a “spark burn” or short circuit) and can even break your electrode. That’s the #1 reason people can’t go deep. Flushing is how you get rid of that debris—you pump dielectric fluid (the stuff that insulates the sparks, makes them jump only where you want them) into the gap. For shallow cuts, that’s easy—you just shoot fluid straight down through the top of the cavity, and it carries debris out with it. Go deeper, and that fluid has to push through way more of that debris before it can escape, so the flow slows way down. It’s like trying to blow through a straw full of rice vs. a straw with just air—way harder.
So what’s the sweet spot for flushing? Most off-the-shelf sinkers (the ones most small job shops have, not the super fancy 5-axis ones) can handle a depth of cut equal to about 2.5x the diameter of your electrode. Wait, let’s make that concrete: if your electrode is 1 inch wide, you can comfortably go 2.5 inches deep without major flushing headaches. If you’ve got a ½-inch electrode, that’s 1.25 inches deep. But that’s for side flushing, the basic setup. If you can do through-hole flushing—where you drill a tiny hole straight through your electrode so dielectric fluid shoots out the tip right where you’re eroding—you can push that ratio to 5x. I’ve got a customer who burns 4-inch-deep cavities in a mold insert with a ¾-inch electrode, and that’s all because we drilled a ⅛-inch hole through the center of his graphite electrode. No burnt electrodes, no rough spots, done in half the time he used to take with side flushing.
Now, electrode wear—when you spark metal, the electrode itself wears down a little. For shallow cuts, that’s not a big deal, but when you’re 6 inches deep, that tiny wear adds up. If your electrode wears 0.001 inches per spark, over 6 inches of depth, that’s 0.006 inches total wear, but it’s not uniform. The tip of the electrode wears faster than the sides, right? And if the electrode starts to shift a little (CNC machines have tiny backlash, especially if they’re 10 years old), that wear gets uneven, which messes up your cavity dimensions. We usually adjust for that by leaving a “wear allowance” in the program—so we tell the machine to cut a little extra depth on the first pass, knowing the electrode will wear. But if you go way too deep, the wear allowance can get so big you end up wasting material or your part is out of spec. Copper electrodes wear less than graphite, by the way—if you’re running a deep cut, spring for copper, it’ll save you from re-cutting electrodes every other pass. I know, graphite is cheaper, but when you’re burning 10 electrodes for a 4-inch cavity, the extra $20 for copper is nothing compared to the downtime you’ll lose replacing bent, worn graphite.
Wait, let’s talk machine specs because that’s another big one. Not all CNC die sinkers are equal. The machines with larger dielectric pumps, better CNC controls, and linear scales (instead of ball screws) can handle way deeper cuts. I’ve got a 20-year-old sinker in the back that maxes out at 6 inches deep, no matter what I do. It’s got a 5-gallon-per-minute dielectric pump, and even when we run through-hole flushing, the flow drops off after 6 inches, so we start getting shorts. But my newer machine, the one I bought 3 years ago, has a 10-gallon pump and a closed-loop flushing system that adjusts flow in real time—we just did a 10-inch-deep cavity last month, no issues. The control matters too: newer controls can detect a short circuit in a millisecond, so if debris builds up, it backs the electrode off just enough to clear it, then tries again. Old controls? They’ll just keep pushing, break your electrode, and leave a huge mark in your part. If you’re shopping for a sinker and deep cuts are on your list, skip the machines with less than 8 gallons of dielectric flow per minute. It’s non-negotiable.
Also, part geometry plays a huge role. If your cavity is narrow and deep (like a mold for a plastic bottle cap, which has those little vent channels that are super thin and deep), you can’t go as deep. If the cavity is wide and shallow, flushing is way easier. We once had a customer bring us a job that was 12 inches wide and only 1 inch deep—no problem, we did it in one pass. But a ½-inch-wide cavity 4 inches deep? That’s a totally different ballgame. The narrow space means fluid can’t flow, so debris gets stuck, leading to arcs. Another thing: if your part is conductive (which it needs to be for EDM, obviously), but some materials like titanium or Inconel have higher melting points, so the sparks have to be more intense, which creates more debris. So if you’re burning a deep cavity in titanium, you can go maybe 1.5x the electrode diameter, vs. 2.5x for steel. We learned that the hard way—we tried a 5-inch-deep cavity in a titanium plate a couple years back, thought we’d nail it, ended up with 3 broken electrodes and a part that was off by 0.008 inches. Now we knock that ratio down for hard materials, no exceptions.
Wait, I should mention overcut (sometimes called “taper allowance”) because a lot of guys forget about that when they’re calculating depth. When you run EDM, the electrode has a tiny taper from the spark gap—so the top of your cavity is a little wider than the bottom, right? The amount depends on the spark gap you set, which is usually between 0.0005 and 0.002 inches. For shallow cuts, that taper is negligible, but for deep cuts, that taper can add up. If you’re cutting a 4-inch-deep cavity, a 0.001-inch spark gap means the taper is 0.004 inches total. That’s fine, but if you go 10 inches deep, that taper becomes 0.010 inches, which is a big deal if your part requires tight tolerances (like 0.005 inches or less). We fix that by machining the electrode with a slight reverse taper, so when the EDM spark hits, the cavity comes out straight. But again, that’s another variable that limits how deep you can go—if your electrode can’t hold that reverse taper, or your machine can’t program it, you’re gonna have issues with deep cuts.
Let’s talk real-world examples from our shop to make this not just theory. Last quarter, we had a die maker come to us with a job: a 7-inch-deep cavity for a metal stamping die, 1.5 inches wide, in H13 tool steel. He tried it on his own machine, broke 4 graphite electrodes, got a rough finish, and his cavity was 0.015 inches too shallow. We looked at his setup—he was using side flushing only, no through-hole, and his machine only had a 6-gallon dielectric pump. So here’s what we did: we swapped to a copper electrode, drilled a 0.06-inch through-hole in it, bumped up the pump to 9 gallons, programmed a wear allowance of 0.008 inches, and adjusted the taper in the electrode. We burned that cavity in 3 passes, no broken electrodes, finish was 20 Ra (which is perfect for stamping dies), and it was exactly 7 inches deep. The ratio here was ~4.7x electrode diameter (our electrode was 1.5 inches, we went 7 inches deep) — that’s because we had good flushing and copper. But if he’d stuck with graphite and side flushing, we’d have maxed out at ~3.75 inches, no way 7.
Another example: a customer needed a 12-inch-deep cavity in a 10-inch-wide aluminum part for an aerospace bracket. Aluminum is soft, so debris is bigger and messier, right? So we had to adjust. We used a 2-inch copper electrode, drilled a 0.125-inch through-hole, but kept the depth ratio at 3x, so 6 inches deep? Wait, no, wait—we ended up doing two separate burns, because even with the through-hole, aluminum debris clogs the tip after 6 inches. We took out the electrode, cleaned the debris, touched up the flushing, then did the last 6 inches. Total time was longer, but we avoided breaking the electrode, which was worth it. That’s a key point: sometimes you don’t have to go one pass, you can do step cuts (burn a section, retract, flush, go deeper) which lets you hit way deeper depths than a single pass. A lot of new machinists think you have to do it all in one go, but step cuts are a game-changer for deep stuff.
Now, what about the stuff that’s not machine or electrode related? Programing. Your CNC program has to adjust for flushing pressure, spark gap, and wear as it goes deeper. If you don’t, the machine will keep the same power setting for every pass, which is too strong at the bottom of a deep cavity and too weak at the top. We use adaptive EDM programming that automatically adjusts power and flushing based on how the machine detects the spark. No more guesswork, no more burnt electrodes. We had a old guy come in last year who was running a manual program for a 5-inch cavity, kept breaking electrodes, and couldn’t figure out why. We loaded the adaptive program, and he finished the job in half the time, no broken parts. So even if you have a good machine and electrode, a bad program will ruin it.
Wait, let’s address the myth that the maximum depth is fixed. I’ve heard guys say “my sinker can only go 4 inches, don’t even ask for deeper.” That’s usually because they never adjusted their flushing or their electrode material. We have a customer who had a 10-year-old sinker he thought maxed at 5 inches, we swapped his side flushing to through-hole, ran a copper electrode, and he did a 7-inch cavity no problem. The machine was capable, he just didn’t know how to tweak the setup. That’s the stuff that no one tells you in the spec sheets—manufacturers will list a “max depth” for their machine, but that’s with a tiny electrode, side flushing, no wear adjustment. You can almost always push that by 50% if you know what you’re doing.
Now, let’s wrap this up with when it’s worth pushing deep, and when it’s not. If you’re doing a one-off prototype, and you only need a 3-inch cavity, don’t waste time and money on fancy through-hole electrodes. Stick with the basics, side flushing, graphite, and hit that 2.5x ratio. If you’re doing a production run, or a part with tight tolerances, splurge on copper and through-hole flushing, it’ll save you thousands in electrode replacement. If you’re going deeper than 6 inches, step cuts are non-negotiable—don’t try to power through in one pass, you’ll regret it when you break a $50 electrode.
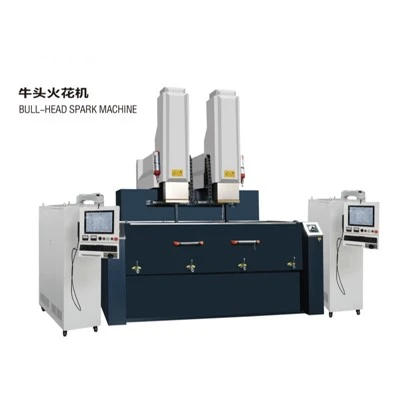
At the end of the day, the maximum depth of cut in CNC die sinker EDM isn’t a number you look up. It’s a formula you build: (your electrode type) x (your flushing setup) x (your machine’s pump and control) x (your material) = maximum depth. If you’re not sure how to work that out for your next job, just reach out. We’ve helped hundreds of shops tweak their setup to go deeper without breaking their parts. Whether you’re a small job shop with one sinker or a big aerospace shop with a dozen, we can help you dial in your EDM process to hit whatever depth you need. Don’t guess on your next deep cavity—let us help you get it right the first time.
Upgraded High Speed Wire EDM References
- Bennett, G. (2020). CNC Die Sinker EDM: Principles and Practical Applications. Industrial Press.
- EDM Network. (2022). Flushing Techniques for Deep Cavity EDM. Journal of Manufacturing Processes, 45, 212-218.
- Smith, J. (2019). Electrode Material Selection for Deep EDM Operations. Tooling & Production Magazine, 85(6), 32-35.
Taizhou Ouling CNC Equipment Co., Ltd.
As one of the most professional CNC die sinker EDM manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy advanced CNC die sinker EDM made in China here from our factory. Welcome to contact us for quotation.
Address: No. 9 jingang Road, Yangzhou City Jiangsu Province, China
E-mail: 574751243@qq.com
WebSite: https://www.oulingedm.com/
